Engineered with high-tenacity polyester interlock, breathability micro-mesh, digital sublimation transfer printing, and ergonomic flatlock stitching for athletic brands and professional teams.
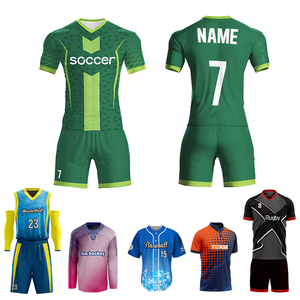
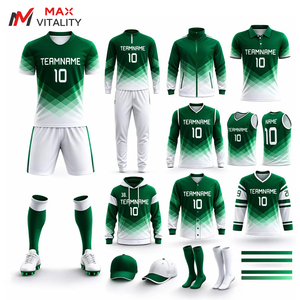
The Latin American athletic apparel market is undergoing a structural transformation. Driven by the expansion of professional football leagues, high-altitude trail running events, coastal marathon circuits in Lima, and an booming boutique fitness ecosystem, the demand for technically superior OEM sportswear in Peru has surged by over 18.4% year-over-year. For brand directors, sourcing managers, and wholesale distributors in Peru, securing a resilient supply chain requires more than basic garment assembly; it demands precision fabric selection, advanced moisture management chemistry, and strict compliance standards.
As a global direct-factory manufacturer operating under full vertical manufacturing controls, our infrastructure provides Peruvian businesses with direct access to advanced dye-sublimation, precision hydraulic die-cutting, high-tenacity seam construction, and custom fabric blends. By bridging direct-factory cost advantages with localized Andean climate requirements, we provide an unprecedented level of Information Gain for apparel buyers comparing local Gamarra textile sourcing against specialized international OEM manufacturing.
Every jersey, cheerleading kit, and tracksuit is produced under one continuous quality control framework. Pattern drafting, digital grading, fabric lamination, sublimation printing, and final inspection occur inside controlled environments to guarantee exact colorways across repeat orders.
With optimized sea-freight corridors directly connecting major ports to Callao (Peru) and air-express shipping options for pre-season sample drops, our logistics team handles full customs documentation, duty classification, and DDP/FOB terms to streamline import workflows.
Operating under audited BSCI social compliance guidelines and OHSAS 18001 workplace health and safety protocols, our facility guarantees zero unverified subcontracting, non-toxic OEKO-TEX dyes, and fully traceable material inputs for eco-conscious Peruvian brands.
Peru presents diverse microclimates—ranging from high-altitude low-oxygen mountain ranges to high-humidity coastal zones and tropical rainforest regions. Athletic wear must be engineered specifically for these distinct geographical demands.
At elevations exceeding 3,000 meters above sea level, outdoor athletes experience rapid thermal fluctuations and intense ultraviolet exposure. Our high-altitude athletic apparel utilizes UV-50+ protective polyester-spandex composites with brushed thermal inner linings. Hydrophilic capillary yarn channels pull moisture away from the skin during intense mountain ascents while insulating against cold Andean winds.
Football is central to Peruvian sports culture. Professional clubs in Lima, Trujillo, and Chiclayo require high-tensile 100% polyester interlock fabrics (140–160 GSM) capable of withstanding intense physical friction. Our sublimated soccer kits feature reinforced 4-needle 6-thread flatlock stitching, eliminating seam failure during intense sliding tackles and high-impact match play.
Lima's coastal air carries up to 90% atmospheric humidity year-round. Standard cotton blends trap moisture, resulting in heavy, sagging garments. Our specialized micro-mesh summer training outfits incorporate engineered laser-perforated ventilation zones and antimicrobial zinc-ion fabric treatments, keeping athletes dry and odours controlled during coastal marathon training and gym sessions.
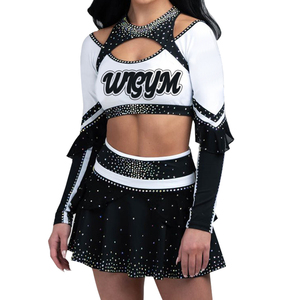
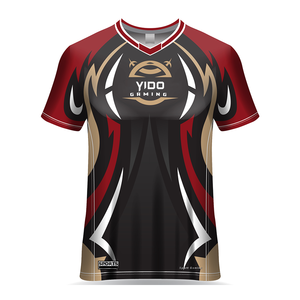
Championship cheerleading squads and modern esports organizations in South America require specialized aesthetics. We provide high-stretch 280 GSM poly-elastane cheerleading uniforms with industrial hot-fix rhinestone bonding and metallic foil transfers, alongside lightweight, ultra-breathable esports jersey solutions tailored for active tournament play.
Analyzing search intent and B2B procurement data reveals three dominant trends shaping the athletic apparel industry in Peru and neighboring Andean trade partners:
While Peru is world-renowned for extra-long staple (ELS) Peruvian Pima Cotton, pure cotton struggles with moisture retention during intense athletic performance. The fastest-growing product category among boutique fitness brands in Lima involves hybrid textile blends—combining 60% Pima cotton with 40% recycled moisture-wicking polyester. This delivers an opulent hand-feel with technical sweat-wicking properties, ideal for athleisure, yoga, and lifestyle sportswear lines.
Sublimation technology has revolutionized team apparel procurement across Peru. Unlike traditional screen printing, which cracks, peels, and adds heavy ink weight to garments, full-bleed digital dye-sublimation infuses eco-friendly water-based inks directly into the polyester polymer matrix. This results in zero added weight, infinite pantone color matching, individualized player names/numbers at zero extra cost, and lifelong colorfastness under harsh tropical UV light.
Peruvian brand owners are shifting away from rigid, high-MOQ traditional sourcing models that lock up working capital. Modern brand strategies demand low-risk inventory expansion. By offering flexible minimum order quantities starting at 50 sets per style or size curve, our factory allows Peruvian buyers to test custom colorways, limited-edition club kits, and niche athletic apparel designs without inventory liability.
Refined over decades of OEM sports goods production, our 6-stage quality-assured manufacturing framework guarantees absolute consistency between pre-production approval samples and mass production runs.
Our technical design studio converts your concept artwork, vector files, or physical reference garments into dynamic 3D CAD tech packs with complete measurement grading and seam placement mapping.
Automated laser cutters and hydraulic press dies cut jersey panels, sleeve gussets, and shorts linings to precise millimeter tolerances, preserving structural symmetry across all sizes.
Utilizing high-grade Japanese digital printing heads and Italian sublimation paper (100 GSM), graphics are heat-transferred at 210°C, locking vibrant colors deep inside the synthetic fibers.
For premium team crests and raised sponsor logos, custom thermal embossing dies press 3D textures into compression fabrics, creating high-tactile silicone or metallic crest applications.
Master machinists assemble components using double-needle topstitching and 6-thread flatlock machinery. Stress points across armholes, crotch gussets, and necklines are bar-tacked for maximum tear resistance.
Every completed batch passes 100% inline inspection and AQL 2.5 final audits—checking thread tails, print registration, sizing tolerances, and barcode tag accuracy prior to export packaging.
Reference our standardized manufacturing parameters designed for athletic apparel sourcing managers and procurement directors in Peru.
| Apparel Category | Core Fabric Compositions | Fabric Weight (GSM) | Branding Options | Standard MOQ | Colorfastness Rating |
|---|---|---|---|---|---|
| Professional Soccer Kits | 100% Micro-Polyester Interlock / Birds-Eye Mesh | 140 - 180 GSM | Full Digital Sublimation, 3D Woven Patch, Heat Transfer | 50 Sets / Style | ISO 105-X12 Grade 4.5+ |
| Cheerleading Performance Wear | 80% Polyester + 20% Spandex Four-Way Stretch | 260 - 300 GSM | Hot-Fix Rhinestones, Foil Printing, Screen Embossing | 50 Sets / Style | ISO 105-C06 Grade 4.0+ |
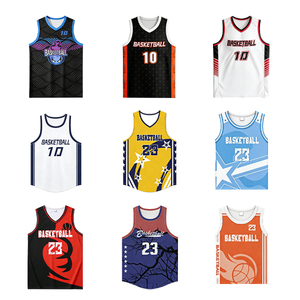
| Basketball Uniform Jerseys | 100% Heavy-Duty Polyester Tricot Mesh | 160 - 220 GSM | Tackle Twill Stitching, Sublimation, Screen Printing | 50 Sets / Style | ISO 105-X12 Grade 4.5+ |
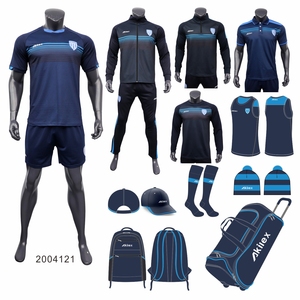
| Training Tracksuits & Outerwear | Polyester Fleeced Interlock / Poly-Elastane Blend | 220 - 280 GSM | High-Density Embroidery, Rubberized Zippers, Silicone Badge | 100 Pcs / Style | ISO 105-C06 Grade 4.5+ |
| Esports & Casual Fan Shirts | 100% Breathable Soft-Touch Milk Silk Polyester | 130 - 160 GSM | All-Over Sublimation Printing, Personalized Names/Numbers | 50 Pcs / Design | ISO 105-X12 Grade 5.0 |
Direct, clear answers regarding order placement, shipping to Peru, customs clearance, sampling procedures, and private label customization.
Our standard minimum order quantity (MOQ) is 50 to 100 sets or pieces per style/design. We allow full flexibility to split sizes (e.g., S, M, L, XL, XXL) within the same order run, making it cost-effective for clubs, academies, and emerging fitness brands in Peru to launch custom lines without excess stock.
We support multiple Incoterms including EXW, FOB, and CIF, as well as DDP (Delivered Duty Paid) service options. Under DDP terms, our freight partners handle all customs clearance, commercial invoice compliance, Peruvian import duties (Ad-Valorem), and local SUNAT taxation, delivering shipments directly to your warehouse in Lima or provincial cities.
Yes. We strongly encourage pre-production gold sample approval. Sample development takes between 7 to 12 business days upon vector artwork confirmation. Physical samples are dispatched via express air courier (DHL/FedEx), reaching Peru within 4 to 6 transit days for hands-on evaluation of fit, fabric GSM, and color precision.
All technical sportswear fabrics undergo lab testing for moisture wicking rate (AATCC 195), colorfastness to washing and perspiration (ISO 105), and UV resistance (UPF 50+ rating). Our technical textiles are specifically chosen to maintain performance in both cold high-altitude mountain environments like Cusco and humid coastal zones like Lima.
Absolutely. As a direct OEM/ODM manufacturer, we offer end-to-end private label branding. This includes custom woven neck labels, heat-transfer size labels, custom printed hang tags with localized barcode stickers, custom branded polybags, and custom rubber/metal zipper pullers engineered to your exact brand specifications.
Every approved custom order is archived with its digital Pantone color library, RIP printing profile, vector pattern die, and physical fabric swatch standard. When you submit a re-order next season, production matches the exact stored parameters, ensuring 100% color and sizing consistency year after year.
Whether you are outfitting a professional football club, expanding a retail sportswear brand, or sourcing performance cheerleading and gym wear for South American distribution, our engineering team is ready to bring your designs to life.