Explore our factory direct, private-label ready athletic equipment and high-performance safety apparel engineered with precision craftsmanship and rigid ISO quality controls.
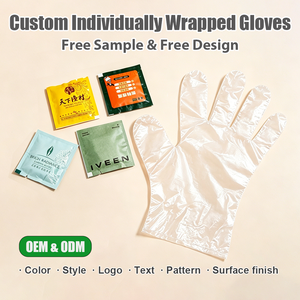
Individually wrapped PE waterproof & oil-proof hygienic gloves engineered for sports nutrition setups, events, and sanitary handling.
Contact Us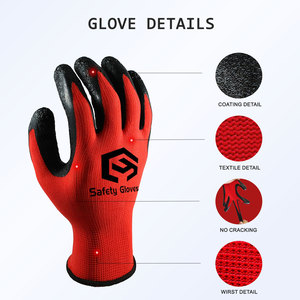
High-tactile grip crinkle latex coated work and facility protection gloves designed for rugged outdoor utility and sports venue maintenance.
Contact Us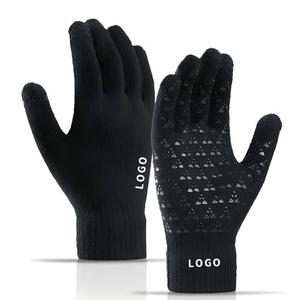
Thermal insulated winter knit activewear gloves featuring conductible fingertip tech and customizable silicone anti-slip palm patterns.
Contact Us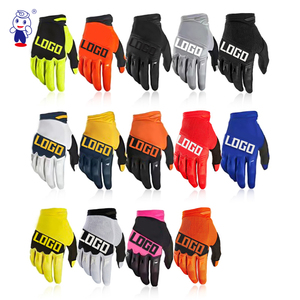
Ergonomic off-road sports gloves built with multi-channel mesh ventilation, impact knuckle guards, and custom sublimated graphics.
Contact Us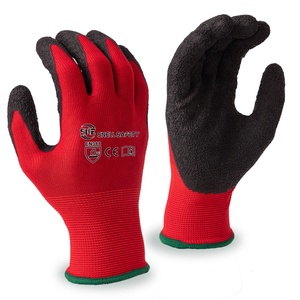
Durable red/black dual-dipped latex coated protection gloves engineered for ergonomic grip during outdoor physical conditioning.
Contact Us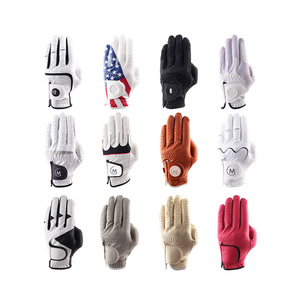
Ultra-soft genuine Cabretta sheepskin combined with breathable PU perforations for Tour-grade feel and customizable brand ball-markers.
Contact Us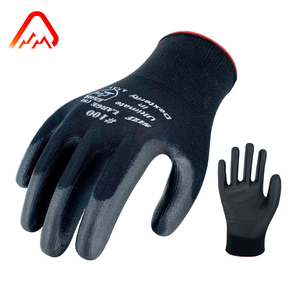
EN388 compliance certified general-purpose athletic utility gloves featuring seamless nylon liners and ultra-thin PU precision palm coating.
Contact Us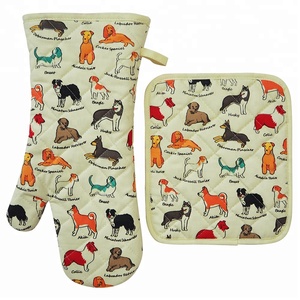
Heavy-duty quilted cotton mitts equipped with heat-resistant silicone printed branding, tailored for high-temperature culinary performance.
Contact UsThe global activewear market has undergone a dramatic structural evolution. Sourcing managers, procurement directors, and D2C apparel founders no longer look solely for low unit prices; they demand uncompromising technical consistency, ethical audit compliance, and end-to-end supply chain transparency. Selecting top trusted custom activewear factories requires an in-depth understanding of material science, pattern grading ergonomics, and factory-level quality assurance protocols.
Established manufacturing centers, notably Sialkot (Pakistan), have established themselves as international powerhouses in precision cut-and-sew apparel, thermo-bonded gear, high-grip latex palms, and technical compression wear. Working directly with vertically integrated factories eliminates intermediary margins, grants direct communication with garment engineers, and guarantees complete control over custom branding specifications—from silicone traction overlays to anti-microbial yarn blends.
How advanced polymer science, ergonomic stitching, and dynamic textile engineering are shaping next-generation activewear manufacturing.
Engineered poly-spandex warp knit structures featuring micro-channel cross-sections that pull perspiration away from epidermis for rapid evaporation during high-intensity training.
German contact latex, dual-dipped crinkle latex, and textured PU palms offering maximum friction coefficients in wet and dry athletic conditions.
High-pressure molecular dye sublimation ensuring vibrant color saturation without clogging fabric pores, complemented by tactile 3D embossed silicone logos.
To assist procurement officers in evaluating order requirements, the technical table below outlines standard performance metrics across our primary OEM/ODM activewear and sports gear manufacturing categories.
| Product Category | Core Material Specification | Standard MOQ | Sample Lead Time | Bulk Lead Time | Quality Standards |
|---|---|---|---|---|---|
| Technical Goalkeeper Gloves | German Contact Latex (3.5mm–4mm) + Neoprene / Breathable Mesh | 100 Pairs / Style | 10 – 14 Days | 25 – 35 Days | EN71 / CE / ISO 9001 |
| Match & Training Soccer Balls | Thermo-Bonded PU / Microfiber Cover + Butyl Bladder | 200 Pcs / Design | 10 – 15 Days | 25 – 35 Days | FIFA Quality Pro Spec |
| Tactical & Safety Work Gloves | 13/15 Gauge Nylon Shell + Crinkle / Smooth Latex Dipping | 500 Pairs / Style | 7 – 10 Days | 20 – 30 Days | CE EN388 (4131X) |
| Cabretta Sheepskin Golf Gloves | AAA Premium Cabretta Leather + Lycra Stretch Inserts | 200 Pairs / Style | 12 – 18 Days | 25 – 30 Days | Tour Grade Inspection |
| Custom Sportswear & Teamwear | 180-240 GSM Poly-Spandex Interlock / Jacquard Mesh | 50 Sets / Style | 7 – 12 Days | 20 – 28 Days | OEKO-TEX Class I |
As global consumer expectations pivot toward sustainability, smart fabrics, and hyper-personalized athletic apparel, procurement strategies must adapt. Sourcing leaders who align with forward-thinking activewear factories gain a massive competitive advantage in speed-to-market and brand trust.
The reliance on virgin petroleum-based synthetics is rapidly diminishing. Leading factories are integrating rPET (recycled polyethylene terephthalate) yarns sourced from ocean-bound plastics, alongside bio-based elastomers and biodegradable packaging films. Supply chains that offer fully certified GRS documentation are becoming default partners for premium activewear brands in North America and Europe.
Traditional factory demands for 3,000+ unit minimums are giving way to dynamic, agile production runs. Advanced computerized die-cutting and automated single-head printing lines allow modern manufacturers to offer flexible MOQs (e.g., 50 to 100 units per style), enabling brands to test limited-edition drops, split size curves dynamically, and avoid overstock markdowns.
Seamless activewear manufacturing reduces fabric waste by up to 35% while eliminating abrasion points across high-friction athletic zones. By utilizing multi-feed circular knitting machinery, manufacturers can seamlessly weave targeted breathability zones, core compression support, and multi-tone aesthetic designs into a single continuous garment panel.
Rooted in Sialkot’s legendary industrial heritage, Spogen Pvt Ltd operates as a premier B2B sports goods and activewear manufacturer. We combine time-honored artisanal seamstress techniques with modern manufacturing automation to serve global apparel brands, professional sports clubs, and industrial distributors worldwide.
Zero middleman markups. From yarn selection and fabric knitting to screen printing, embroidery, and final carton packing, every stage is controlled inside our audited Sialkot facility.
Our operations comply with stringent social responsibility, fair wage policies, workplace health, and environmental safety guidelines, ready for third-party brand audits.
Complete custom branding options including custom heat-transfer neck tags, woven hem labels, custom barcode polybags, and custom retail presentation boxes.
Here are detailed answers to the most common questions raised by sourcing managers, brand owners, and supply chain directors during factory evaluation.
Our standard MOQ starts at 50 pieces per style for sublimated teamwear and activewear kits, 100 pairs per model for specialized gloves (goalkeeper/golf), and 200 pieces for inflatable match balls. Flexible color and size breakdowns are accommodated within the total order volume.
Pre-production physical samples are crafted within 7 to 18 working days post artwork and tech-pack approval. Samples are sent via express air courier (DHL/FedEx) alongside material swatches and gold-sample sign-off sheets for formal buyer approval prior to bulk production launch.
Absolutely. We regularly sign binding Non-Disclosure Agreements (NDAs) to protect proprietary pattern geometry, custom fabric developments, and client brand artwork. Your designs are strictly reserved for your exclusive production runs and never repurposed.
We support FOB (Sialkot/Karachi), EXW, CIF, and DDP (Delivered Duty Paid) shipping terms via sea freight, air cargo, and courier express. Accepted payment structures include Wire Transfer (T/T), Irrevocable L/C at sight, and flexible milestone terms for established long-term accounts.
Every finalized order is archived with its master digital CAD pattern, fabric lot swatch, ink mixing formula, and physical gold sample. Subsequent reorders are matched against these stored parameters and subjected to identical inline AQL 1.5/2.5 inspection routines.
Partner with a certified, trusted activewear supplier. Contact our engineering and sales teams to submit your tech packs, request sample swatches, or schedule a virtual factory walk-through.
Contact Us