Engineered for global brands, athletic clubs, and commercial distributors with strict quality assurance and flexible MOQ structure.
Annual Unit Production
Social Compliance Audited
Rigorous Inspection Standard
Global Destination Markets
The global custom teamwear and athletic gear industry is undergoing a paradigm shift driven by digital sublimation tech, sustainable fabric blends, strict international compliance protocols, and accelerated supply chain timelines. As international sport brands, athletic clubs, and corporate buyers evaluate their global sourcing footprint, China remains the foundational center of gravity for advanced technical textile manufacturing, specialized protective gear development, and end-to-end contract assembly.
In this technical white paper, we outline the engineering metrics, sourcing paradigms, compliance frameworks, and future material trends that govern modern high-volume teamwear and specialized glove production. By bridging factory-floor material science with real-world procurement demands, our manufacturing facility provides sports brands and wholesale buyers with unmatched technical authority and predictable product replication.
Strategic Sourcing Note: Direct-from-factory OEM programs cut intermediary margin stack-ups by 18% to 32% while providing direct access to technical material specifications, custom pattern grading, and rigorous quality control trace reports.
High-performance teamwear requires meticulous engineering across all production stages. Achieving superior moisture management, color fastness, mechanical elasticity, and durability under competitive conditions requires holistic integration of textile engineering and automated fabrication.
Modern athletic uniforms rely on multi-filament synthetic compositions specifically structured for high tensile strength and rapid sweat evaporation:
Traditional screen printing alters the tactile permeability of performance fabrics. Our factory utilizes high-definition digital sublimation systems utilizing Japanese eco-solvent inks bonded at 210°C under industrial pressure. This molecular dye infusion ensures that team logos, sponsor graphics, and pantone matched gradients will never crack, peel, or fade, maintaining 100% breathability across the entire textile area.
Automated optical camera laser cutters cut fabric panels to within 0.5mm precision, eliminating raw edge fraying and guaranteeing strict sizing consistency across thousands of kit items.
6-needle 4-thread flatlock stitching reduces seam bulk and inner garment friction, preventing skin abrasion during prolonged athletic movement.
Full social accountability auditing, clean working conditions, fair wage standards, and environmental management frameworks certified for global retail entry.
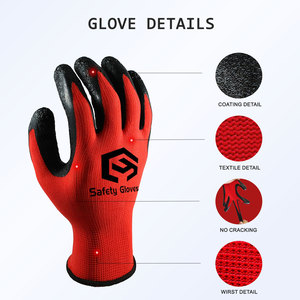
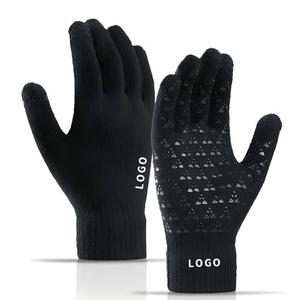
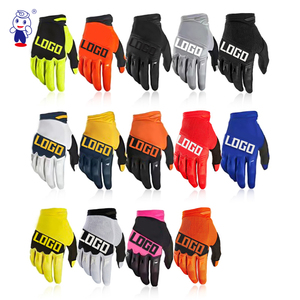
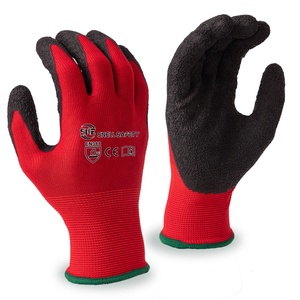
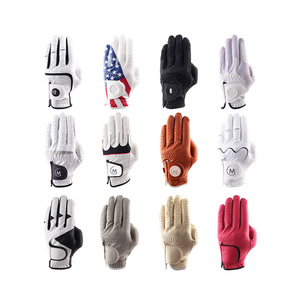
Beyond sports apparel, specialized glove manufacturing requires intricate material layering and vulcanization techniques. Whether crafting professional golf gloves, CE-certified work gloves, or high-performance motorcycle racing gear, material selection dictates dynamic user protection.
| Glove Category | Primary Material Compound | Performance Certification / Test | Key Engineering Attribute |
|---|---|---|---|
| Golf & Tactical Gloves | Premium Cabretta Sheepskin / Ultra-thin PU | ISO 20344 Friction Index | Anatomical 0.45mm skin feel with moisture-wicking knuckle perforations. |
| Industrial Work Gloves | 13-Gauge HPPE / Crinkle Latex & PU Dip | EN388 (4544D Cut Level) | High abrasion, oil resistance, and ergonomic grip for heavy construction. |
| Motorcycle & Sports Gloves | Sublimated Air-Mesh + Carbon Fiber Knuckle | CE EN 13594 Impact Protection | Anti-vibration foam padding, pre-curved fingers, high-velocity abrasion mesh. |
| Thermal & Winter Gloves | Conductive Touchscreen Fiber + Thermal Knit | EN 511 Cold Protection | 10-finger capacitive response with windproof inner thermal barrier. |
Navigating global supply chain volatility requires forward-looking market intelligence. Over the next decade, wholesale teamwear procurement will be shaped by four transformative vectors:
The era of requiring 5,000-unit minimums per SKU is rapidly closing. Brands require agile manufacturing models capable of executing 50 to 200 unit customized team kits with speed. Modern factories utilize digital pattern generation and modular assembly lines to make short-run custom orders commercially viable without inflated unit costs.
European and North American import regulations (such as EU Digital Product Passports) are mandating full supply chain transparency. Future teamwear contracts will prioritize factories utilizing solution-dyed yarns (which reduce water consumption by 80%), biodegradable PE packaging, and verified post-consumer recycled fabrics.
Post-pandemic health consciousness has elevated functional fabric finishes. Silver-ion anti-bacterial treatments integrated directly into polyester fibers permanently prevent odor-causing bacteria growth. Simultaneously, phase-change materials (PCM) embedded into compression baselayers actively absorb and release body heat to regulate body temperature during elite competition.
Procurement departments are replacing manual PDF spec sheets with direct 3D CAD pattern rendering. This allows brand managers to visualize stress points, sublimation graphic alignment, and seam stretch before physical sampling, cutting pre-production sample rounds from three iterations down to one.
When sourcing custom teamwear and technical gloves from China, choosing a direct manufacturing facility over trading intermediaries offers critical strategic advantages:
Clear answers to technical specifications, order logistics, sampling, and global export compliance.
Connect directly with our engineering and merchandising team to discuss technical specs, request material sample cards, or obtain a competitive factory-direct quote.
Inquire Now