Precision-engineered apparel manufactured using advanced circular knitting, 4-way stretch compression fabrics, and ergonomic flatlock stitching.
Engineered with 300 GSM Polyamide-Elastane blend, squat-proof opacity, and targeted micro-ventilation zones for extreme training support.
Contact Us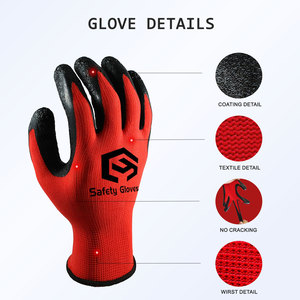
Constructed from featherweight 140 GSM hydrophobic polyester, featuring antimicrobial yarn treatment and rapid vapor dispersion weave.
Contact Us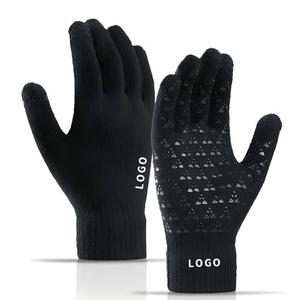
Features conductive fingertips, brushed thermal jersey lining, and anti-slip silicone palm mapping for outdoor athletic disciplines.
Contact Us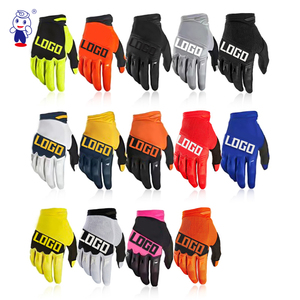
Offers maximum kinetic stability, bounce reduction, laser-cut ventilation apertures, and moisture-wicking double-layer chest banding.
Contact Us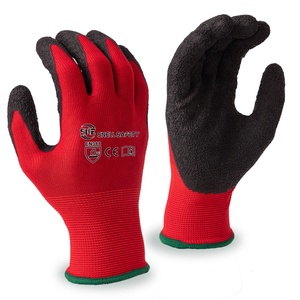
Reinforced double-stitched cotton webbing with neoprene wrist padding designed for high-tonnage deadlift and bodybuilding applications.
Contact Us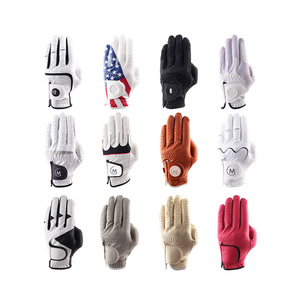
Tactile grade genuine sheepskin and synthetic leather hybrid glove featuring breathable lycra finger gussets and padded palm protection.
Contact Us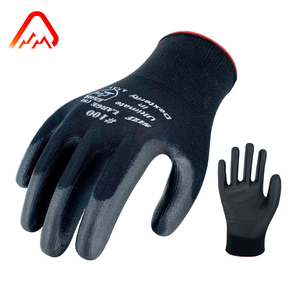
Compliant with CE EN388 friction standards, incorporating textured polymer grip mapping for functional cross-training and powerlifting.
Contact Us
Insulated cotton-polyester matrix designed for localized thermal retainment, post-workout muscle warming, and recovery compression.
Contact UsIn the rapidly expanding global fitness market, selecting a top China gym apparel supplier & exporter requires an in-depth evaluation of vertical manufacturing capabilities, textile engineering expertise, supply chain transparency, and rigorous quality control protocols. Modern activewear has evolved from basic cotton gym tops into highly engineered functional wear that combines advanced polymer composition, biomechanical support, dynamic moisture vapor management, and circular sustainability metrics.
As a leading OEM/ODM manufacturing facility in China, our infrastructure integrates high-gauge circular seamless knitting machinery, automated laser cutting tables, eco-friendly dye houses, and state-of-the-art testing laboratories. We empower global private labels, activewear conglomerates, and digital-native fitness brands to deliver high-margin, ultra-durable, and aesthetically flawless sportswear lines to international retail markets.
Our manufacturing enterprise is structured to eliminate supply chain friction, optimize production lead times, and guarantee batch-to-batch consistency. Our factory operations leverage industry 4.0 smart manufacturing principles across four dedicated production workshops:
Equipped with 28G to 34G Santoni circular knitting machinery capable of producing gradient compression zones, integrated mesh breathability structure, and zero-waste garment bodies.
Operates under audited BSCI social compliance, SMETA 4-Pillar, ISO 9001 quality management, and OEKO-TEX Standard 100 non-toxic raw material certification frameworks.
End-to-end supply chain execution including EXW, FOB, CIF, and DDP solutions with customs clearance support across Europe, North America, Oceania, and the Middle East.
The performance of gym apparel is fundamentally dictated by yarn selection, textile construction, and chemical finishing processes. Modern fitness enthusiasts require activewear that withstands repeated high-tensile stress, offers optimal thermoregulation, and retains color vibrancy after hundreds of wash cycles.
Our R&D team continuously innovates with composite blends including Polyamide 6.6 (Nylon 66) for high abrasion resistance, micro-denier Polyester for rapid wicking, and high-purity Elastane (Spandex) for dynamic 4-way elastic recovery. Below is a technical breakdown of our proprietary activewear fabric formulations available for custom OEM production:
| Fabric Composition | GSM Weight | Stretch & Recovery | Moisture Management | Target Gym Application |
|---|---|---|---|---|
| 80% Nylon / 20% Elastane | 220 - 310 GSM | 4-Way Stretch (>220% elongation) | Hydrophilic wicking finish | Squat-proof leggings, shapewear, compression tops |
| 88% Recycled Poly / 12% Spandex | 160 - 240 GSM | 4-Way Stretch (>180% elongation) | Rapid vapor evaporation weave | Athletic training tees, gym shorts, running vests |
| 92% Polyamide / 8% Elastane (Seamless) | 280 - 350 GSM | Zonal Compression Mapping | Micro-porous airflow structure | Seamless sports bras, seamless contours, crop tops |
| 75% Micro-Nylon / 25% Spandex (Brushed) | 210 - 260 GSM | Ultra-soft 2nd-Skin Feel | Double-sided thermal wicking | Yoga wear, leisure fitness sets, lounge activewear |
| 100% Cationic Polyester Mesh | 120 - 150 GSM | 2-Way Mechanical Stretch | Extreme breathability grid | High-intensity cardio tanks, ventilated paneling |
As global brands evaluate their activewear procurement strategy, shifting consumer demands and regulatory frameworks are redefining the manufacturing landscape. Procurement managers must align with forward-thinking China gym apparel suppliers who actively implement the following technical and operational trends:
Environmental compliance has shifted from a marketing niche to a baseline requirement. Global markets, particularly the EU and North America, are enforcing strict carbon accounting and trace-to-origin mandates. Future-proof gym apparel relies heavily on GRS-certified Recycled Nylon (made from ocean ghost nets and textile waste) and Global Recycled Standard (GRS) Recycled Polyester (rPET). Furthermore, plant-based water-repellent treatments and bio-based elastomers are rapidly replacing traditional fossil-fuel derived spandex.
Traditional cut-and-sew garment manufacturing yields between 15% to 25% fabric scrap waste. The future of athletic apparel manufacturing belongs to 3D circular seamless knitting. By knitting tubular garment blanks directly from raw yarn bobbins, material utilization exceeds 96%. This not only significantly reduces environmental impact but also eliminates chafing seam lines, delivering superior tactile comfort for endurance athletes.
Next-generation gym wear integrates varying tension densities directly into the fabric structure. By altering stitch patterns, suppliers can offer target support to muscle groups—such as quadriceps stabilization, lumbar support, and core compression—without adding extra sewn panels. Additionally, the integration of far-infrared (FIR) emitting bio-ceramic yarns facilitates enhanced micro-circulation and accelerated post-workout muscle recovery.
To mitigate inventory holding costs and overproduction risks, global fitness brands are moving away from massive seasonal inventory dumps toward agile, multi-batch reorder models. Top Chinese exporters are adopting digital sublimation print houses, automated fabric spreading, and flexible modular assembly lines that accommodate low Minimum Order Quantities (MOQs) for limited-edition color drops while maintaining bulk scale economics.
Designing a bestselling activewear line requires a deep understanding of market trends and functional performance requirements. When partnering with an OEM supplier, brand owners should incorporate the following product development features into their tech packs:
To assist procurement directors, sourcing agents, and brand founders in navigating the OEM manufacturing process, we have compiled detailed answers to the most frequent technical inquiries:
For standard cut-and-sew activewear using stocked colors, our standard MOQ is 100 pieces per style/colorway across a full size curve. For custom pantone-dyed fabrics or custom seamless knitted styles, the standard MOQ ranges from 300 to 500 pieces per colorway depending on fabric GSM and yarn technical specs.
Pre-production sample creation typically takes 7 to 12 business days upon digital tech pack and artwork sign-off. Once pre-production gold samples are approved, bulk manufacturing requires 25 to 35 business days, depending on order volume, complex branding (embroidery, heat transfer, silicone print), and laboratory testing schedules.
We utilize computerized Datacolor spectro-photometers to establish precise Lab color values. Bulk dye lots are matched against approved Pantone TPX/TCX references with a Delta E (ΔE) tolerance of less than 0.8. All fabric rolls undergo standardized inspection under daylight (D65) and retail store lighting environments prior to cutting.
Our quality management system follows the international ISO 2859-1 (ANSI/ASQ Z1.4) Single Sampling Plan using Quality Limit AQL 1.5 for critical/major defects and AQL 2.5 for minor defects. Every order undergoes 100% inline inspection during seam sewing, followed by final AQL carton sampling before sealing.
Yes, our in-house fashion engineering team can translate physical samples, hand sketches, or mood boards into commercial CAD tech packs. We offer complete turnkey branding packages including woven neck labels, heat-transfer wash tags, TPU rubber badges, custom silicone waist grips, hangtags, and biodegradable zipper polybags.
We support all standard Incoterms 2020 including EXW, FOB (Ningbo/Shanghai/Shenzhen), CIF, CFR, and hassle-free DDP (Delivered Duty Paid) via express air freight or ocean container, delivering goods directly to your Amazon FBA fulfillment center or private logistics warehouse.
Establishing a successful activewear brand demands a supplier that offers far more than basic sewing capacity. You need a dedicated manufacturing partner invested in your long-term market growth. By bridging advanced material science, rigorous European audit standards, competitive Chinese factory-direct pricing, and uncompromised quality assurance, we stand as the top choices for global fitness apparel brands.
Whether you are scaling an established athletic label or launching a high-performance activewear startup, our engineering team is ready to transform your performance apparel visions into market-ready commercial reality.
Contact our engineering and sales merchandising team today to receive a instant quote, order custom fabric swatches, or initiate pre-production sampling for your next activewear collection.
Contact Us