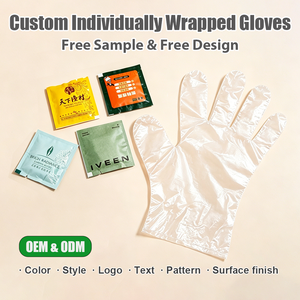
Custom Single Use PE Waterproof Food & Hospitality Gloves
- High-Density Polyethylene (HDPE/LDPE)
- Waterproof & Oil-Resistant Barrier
- Individually Wrapped Takeout Packaging
Inspected under ISO 9001 & BSCI standards. Custom artwork, flexible MOQs, private labeling, and worldwide DDP export support.
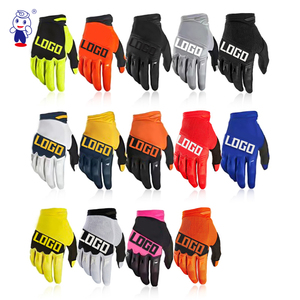
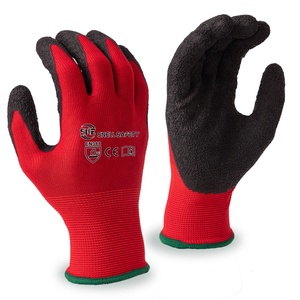
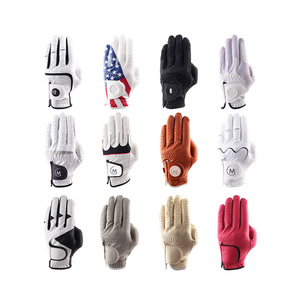
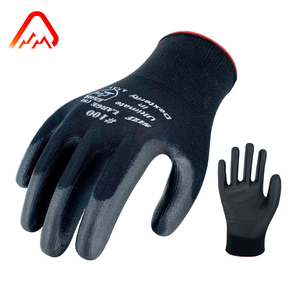
The global sports equipment supply chain is experiencing a structural paradigm shift. According to recent international trade data, demand for high-performance athletic gear, custom protective equipment, and specialized sporting apparel is projected to expand at a CAGR of 6.8% through 2030. Enterprise procurement officers and brand directors must navigate complex geopolitical dynamics, evolving material compliance regulations, and escalating consumer demands for eco-friendly manufacturing.
Key manufacturing clusters, particularly historic industrial centers like Sialkot, Pakistan, continue to command a dominant global market share in hand-stitched and thermo-bonded match balls, premium German-latex goalkeeper gloves, custom sportswear, and specialized tactical gear. By combining traditional craftsmanship with modern automated die-cutting, ultrasonic bonding, and digital sublimation printing, direct sports equipment factories offer unprecedented margins and precision tolerances for international wholesale buyers.
How enterprise buyers are restructuring their vendor evaluation criteria to mitigate risk and boost profit margins.
Shift toward recycled TPU, solvent-free PU coatings, bio-based latex foams, and GRS-certified recycled polyester. Regulatory pushes in North America and Europe mandate strict REACH and RoHS chemical compliance.
Brands require agile manufacturing models to prevent overstocking. Modern OEM factories accept split size-curves and multi-colorway allocations within a single production master run.
Ethical labor standards, fair wage verification, and OHSAS 18001 occupational safety compliance have evolved from optional corporate social responsibility goals into mandatory vendor qualification prerequisites.
Selecting the right manufacturing partner requires rigorous technical evaluation. Below is an insider benchmark matrix used by top-tier sporting goods sourcing directors:
| Evaluation Parameter | Middleman / Trading Office | Direct OEM Factory (e.g., Spogen Hub) | Impact on Enterprise Buyers |
|---|---|---|---|
| Pricing Structure | 15% - 35% Middleman Markup | Direct Factory Floor Costs | Maximizes Gross Profit Margins |
| Quality Assurance | Outsourced Random Sampling | In-House Inline & AQL 2.5 Inspection | Zero Batch Contamination & Low Return Rates |
| Custom Prototyping | 21 - 35 Days (3rd Party Friction) | 7 - 18 Days (In-House Patterning) | Faster Time-To-Market for Seasonal Lines |
| Traceability & Audit | Opaque Supply Network | Full BSCI & OHSAS Transparency | Total Compliance Security & Brand Protection |
| Reorder Consistency | Variable Supplier Sourcing | Archived Tooling, Dies & Color Codes | Identical Material Standards Season-after-Season |
Headquartered in Sialkot, Pakistan—the world's capital of sports gear manufacturing—Spogen Pvt Ltd stands as an audited BSCI and OHSAS 18001 certified B2B manufacturing partner. Operating with comprehensive in-house production capabilities across four core divisions (Goalkeeper Gloves, Soccer Balls, Custom Sports Bags, and Technical Apparel), Spogen eliminates traditional trading agency friction by providing direct access to factory floor engineering.
Automated presses cut German latex palms, leather panels, synthetic rubbers, and heavy-duty 1600D Cordura fabrics to millimeter tolerances.
High-pressure thermal embossing creates raised tactile textures, 3D backhand strike zones, silicone grip surfaces, and durable anti-peel brand logos.
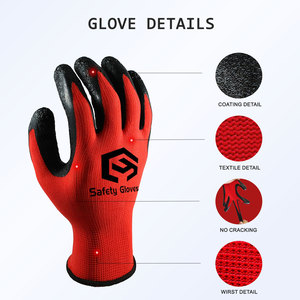
From seamless match balls with zero water absorption to reinforced safety gloves with Kevlar thread, automated assembly ensures peak structural integrity.
Complete turn-key customization including woven neck labels, hang tags, barcode stickers, printed polybags, and retail packaging display boxes.
Answers to essential technical and commercial questions raised by international procurement teams.
Our flexible MOQ structure is designed to support both boutique athletic brands and established enterprise distributors. Typical MOQs are 100 pairs per model for Goalkeeper Gloves and Safety Gloves, 200 pieces per design for Soccer Balls, 100 pieces per style for Custom Sports Bags, and 50 sets per size-curve for Technical Sportswear. Mixed colorways and size splits can be accommodated within a single master production order.
Pre-production gold samples are generated within 7 to 18 working days following CAD artwork approval and physical material selection. Once the pre-production sample is approved in writing by the client, full bulk manufacturing typically takes 20 to 35 working days, depending on batch complexity and branding methods. Worldwide shipping can be organized via sea freight, air freight, or express courier services under DDP, FOB, or EXW terms.
All safety gloves, industrial work mitts, and protective sporting wear undergo rigorous in-house testing for abrasion resistance, blade cut resistance, tear strength, and puncture force. Raw materials are pre-tested to ensure conformity with EN388 mechanical safety directives and CE certification guidelines prior to full-scale assembly.
Yes. We offer complete private label production services. This includes custom woven neck/side tags, high-definition embroidered or silicone logos, custom printed retail header cards, SKU barcoding stickers, and retail-ready polybags or corrugated display boxes suited for immediate distribution center intake.
Every approved custom programme is stored in our digital product archive. We maintain master physical die patterns, pantone color recipes, material specification master sheets, and signed physical gold samples. Subsequent reorders are produced against these archived parameters and inspected to the exact recorded baseline, ensuring perfect long-term product consistency.
Our manufacturing plant operates strictly within the BSCI (Business Social Compliance Initiative) framework and OHSAS 18001 occupational health and safety systems. Qualified enterprise buyers are welcome to request audit reports or conduct independent third-party factory audits during vendor onboarding.