Explore our top-tier OEM/ODM performance collection featuring engineered fabrics, high-grip ergonomics, and military-grade durability produced in our BSCI & OHSAS 18001 audited facilities.
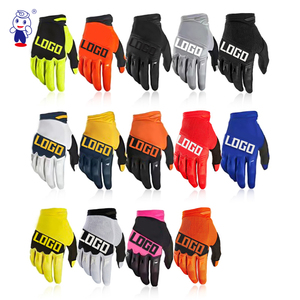
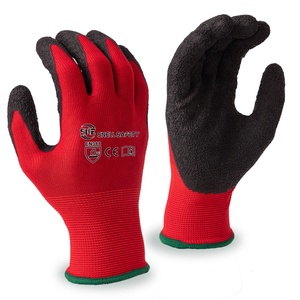
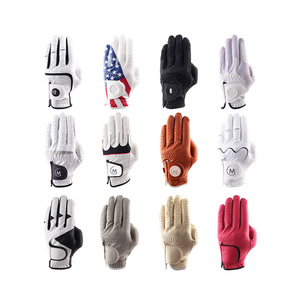
Global activewear consumption is projected to eclipse $450 Billion by 2028. Sourcing leaders must navigate volatile supply chains, strict ESG directives, and evolving consumer intent for multi-functional athleisure. This white paper breaks down top-tier manufacturers and key industry metrics.
Evaluated on operational transparency, technical knitting capabilities, minimum order flexibility (MOQ), international certifications, and R&D capability.
Core Specialization: Custom Technical Activewear, Performance Goalkeeper Gloves, Seamless Teamwear & Sports Gear.
Spogen stands out as a premier OEM/ODM direct manufacturer operating from Sialkot's world-renowned manufacturing cluster. Unlike traditional trading houses, Spogen manages 100% in-house production ranging from hydraulic die-cutting and 3D embossing to sublimation printing and final AQL inspection. Holding strict BSCI social compliance and OHSAS 18001 certifications, Spogen provides flexible MOQs (100–200 units) paired with enterprise-grade quality guarantees.
Core Specialization: High-Volume Knitted Activewear & Athletic Fleece.
As one of the world’s largest vertical apparel manufacturers, Shenzhou operates massive facilities across China, Vietnam, and Cambodia. They serve top global athletic brands with unmatched capacity, specialized yarn spinning, and large-scale fabric knitting, though minimum order quantities typically require enterprise-level volume commitments.
Core Specialization: Advanced Functional Fabrics & Elastic Knitwear.
Eclat is renowned for its synthetic yarn research and elastic fabric engineering. They provide proprietary moisture-management and ultra-flexible compression textiles utilized by high-end athleisure brands demanding premium material hand-feel.
Core Specialization: Seamless Activewear & Ultrasonic Bonded Apparel.
Regina Miracle utilizes advanced 3D CAD molding, laser cutting, and stitchless bonding technology. Their product lines excel in high-impact sports bras, seamless leggings, and friction-free performance baselayers.
Core Specialization: Seamless Bodywear & Targeted Compression Gear.
Operating global manufacturing hubs, Delta Galil specializes in seamless circular knitting technology that creates zoned ventilation and variable compression levels within a single continuous garment.
Core Specialization: Technical Outerwear & Weatherproof Performance Wear.
Maxport specializes in complex construction activewear, including seam-sealed outerwear, thermal running jackets, and technical windbreakers manufactured under stringent environmental controls.
Core Specialization: Outdoor Athletic Apparel & Insulated Sportswear.
A long-standing global titan in functional outdoor and athletic gear, Youngone operates massive production networks in Bangladesh and Vietnam with expertise in down fill, membrane lamination, and synthetic insulation.
Core Specialization: Precision Workmanship & Extreme Sports Apparel.
Focused on high-complexity, low-margin-of-error activewear such as cycling bibs, alpine wear, and triathlon suits. KTC prioritizes master tailoring and mechanical performance over raw mass volume.
Core Specialization: Multi-Category Sportswear & Lifestyle Athleisure.
Crystal operates an expansive multi-country co-creation model, delivering scalable denim, sportswear, and casual athletic knits with automated cutting and digital print integration.
Core Specialization: End-to-End Fashion Athletic Apparel Supply Chain.
Luen Thai operates global apparel manufacturing facilities combined with design services, serving major global activewear brands through lean manufacturing and integrated logistics solutions.
Strategic benchmark comparing key sourcing regions across lead times, MOQ flexibility, technical complexity, and compliance governance.
| Manufacturing Region | Typical MOQ | Sample Turnaround | Primary Technical Advantage | ESG & Compliance Index |
|---|---|---|---|---|
| Pakistan (Sialkot Hub) | 100 - 300 Pcs | 7 - 14 Days | Custom Stitching, German Latex, Sublimation & Sports Gear | High (BSCI / OHSAS 18001 / ISO Certified) |
| China (Guangdong/Zhejiang) | 500 - 1,000 Pcs | 10 - 20 Days | Mass Synthetic Supply Chain & Raw Material Sourcing | Variable (Requires On-Site Audits) |
| Vietnam | 1,000+ Pcs | 15 - 25 Days | Large-Scale Assembly & Bonded Outerwear | High (WRAP / HIGG Index / SMETA) |
| Turkey | 300 - 500 Pcs | 10 - 15 Days | Cotton-Blend Athleisure & Proximity to European Logistics | Medium-High (OEKO-TEX / GOTS) |
How forward-thinking B2B buyers are altering their activewear procurement strategies for 2026 and beyond.
Sourcing departments are moving rapidly from virgin polyester to GRS-certified recycled PET derived from ocean plastics, alongside bio-based nylon synthesized from castor oil to meet corporate carbon reduction targets.
To reduce excess inventory risk, procurement leads are replacing massive annual bulk purchase orders with flexible, small-batch initial orders (100–300 pcs) backed by rapid 20-day reorder cycles.
3D garment simulation tools (Clo3D / Browzwear) enable manufacturers to issue accurate digital pre-production proofs within 48 hours, trimming weeks off standard sampling timelines and reducing textile waste.
Analysis of changing end-user preferences driving technological innovations in functional sportswear design.
Consumers expect seamless wearability that prevents chafing during high-intensity training. Advanced circular knitting machines now allow manufacturers to engineer high-compression zones around key muscle groups while keeping breathability panels over high-heat areas in a single garment cut.
The boundary between sportswear and lifestyle apparel has dissolved. Modern activewear must offer high moisture vapor permeability, anti-odor silver ion treatments, and 4-way elastic recovery while retaining a sleek, polished aesthetic suitable for everyday wear.
Single-site quality management, direct factory pricing, and rigorous compliance documentation give brands a key competitive advantage.
No trading intermediaries or hidden subcontracting. Every stage from raw fabric cutting to stitching and packaging is executed in audited facilities.
Support for startup collections and established brand line extensions with low MOQs, custom woven labels, silicone branding, and retail box packaging.
Mass production runs are strictly locked against physically signed pre-production samples and documented specification sheets to ensure color fastness and sizing consistency.
Established freight forwarding channels across the US, UK, EU, Australia, and Gulf markets under EXW, FOB, or door-to-door DDP arrangements.
Key operational, technical, and logistics queries answered for B2B procurement managers.
Connect directly with our factory merchandising team today. Receive instant feedback on your design tech packs, material availability, and competitive wholesale pricing.