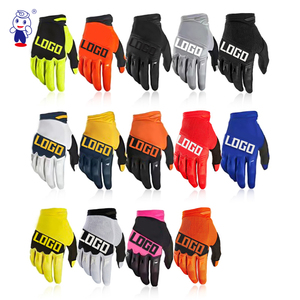
Engineered for global athletic brands, high-performance club teams, commercial distributors, and industrial safety lines. All items are open for custom logo, technical material spec tweaking, and full OEM packaging.
Executive Summary: As global athletic brands navigate dynamic macroeconomic shifts, consumer demands for eco-friendly performance fabrics, and tight delivery schedules, selecting a qualified B2B OEM manufacturing partner in China is paramount. This technical procurement report outlines critical parameters for evaluation, material innovations, supply chain resilience, and compliance benchmarks for decision-makers in 2025 and beyond.
The global activewear market has evolved from simple cut-and-sew operations into a highly sophisticated interplay of textile polymer chemistry, ergonomic biomechanics, and digitalized supply chain execution. Modern sportswear manufacturing demands stringent control over dynamic stretch recovery, thermal regulation, hydro-phobic permeability, and seam tensile tolerance. B2B buyers must partner with manufacturers that possess vertically integrated capabilities—from yarn extrusion and circular knitting to automated laser cutting, seamless bonding, and certified AQL quality control.
China remains the undeniable global epicenter for technical activewear production, offering unparalleled industrial cluster depth. From premium microfiber nylon formulation to specialty polyurethane coatings and elastane blending, Chinese manufacturing hubs provide end-to-end supply chain agility that minimizes lead times while maximizing cost efficiency per SKU.
International sourcing compliance is no longer optional; it is a fundamental prerequisite for global retail distribution. Leading OEM exporters operate under internationally audited management systems including BSCI (Business Social Compliance Initiative), ISO 9001:2015 Quality Systems, and OHSAS 18001 / ISO 45001 Occupational Health & Safety Frameworks.
Our manufacturing ecosystem enforces strict batch traceability across every production step. Raw fabrics undergo continuous testing for colorfastness under perspiration (ISO 105-E04), dimensional stability after washing, abrasion resistance (Martindale test), and tensile elongation. Furthermore, activewear designed for international export adheres to REACH regulation guidelines and OEKO-TEX Standard 100, ensuring complete freedom from harmful chemical residues, heavy metals, or hazardous azo dyes.
Compare core technical fabrics and polymer coatings utilized in our high-performance sportswear, activewear accessories, and specialized protective lines.
| Material / Textile Grade | Composition & Construction | Key Performance Indicators | Primary Activewear / Gear Application | Eco-Compliance Standard |
|---|---|---|---|---|
| Recycled GRS Polyester | 88% rPET / 12% Elastane Interlock (240-300 GSM) | Moisture Wicking, RET < 6, UPF 50+ UV Shield | Compression Wear, Athletic Tops, Leggings | GRS Certified, OEKO-TEX 100 |
| High-Tenacity Micro-Nylon | 80% Nylon 6,6 / 20% Spandex Warp Knit | Abrasion Resistance > 50k Rubs, 4-Way Stretch | Pro Cycling Kits, Compression Gear, Gymwear | REACH Compliant, Bluesign Approved |
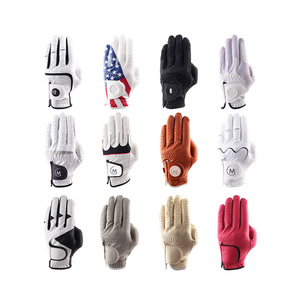
| Cabretta Leather & Synthetic PU | 0.45mm Cabretta Sheepskin / Microfiber Base | Tactile Sensitivity, Wet/Dry Grip Coefficient 0.85 | Professional Golf Gloves, Equestrian Gear | LWG (Leather Working Group) Certified |
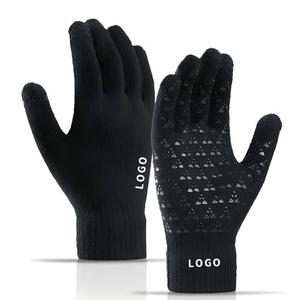
| Seamless 3D Knitted Thermal Fiber | Polyamide / Acrylic / Touchscreen Conductive Thread | Thermal Insulation (CLO 1.2), Capacitive Touch | Winter Running Gloves, Thermal Underlayer | RoHS / CE Certified |
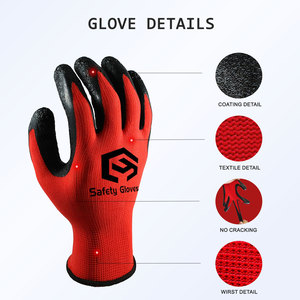
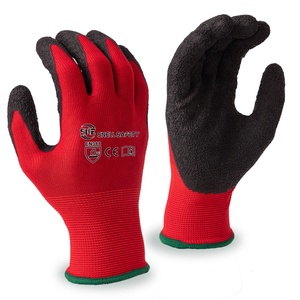
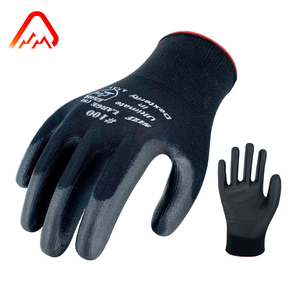
| EN388 Micro-Foam Nitrile/PU | 13/15 Gauge Seamless Nylon Liner + Coating | EN388 Cut Level A2-A4, Oil-Resistant Flex | Motorsport Mechanics, Tactical & Outdoor Gear | CE EN388 Approved, ANSI Cut Level |
Stay ahead of global supply chain disruptions and technological evolutions by aligning your product line with next-generation manufacturing trends.
Integration of phase-change materials (PCMs) and graphene-infused fibers that actively regulate micro-climate temperature during high-intensity training.
Transitioning from traditional flatlock stitching to ultrasonic welding and 3D circular knitting, reducing seam friction, weight, and production waste.
Implementation of 100% closed-loop circular textiles, bio-based spandex substitutes, and waterless digital sublimation printing inks.
Leveraging 3D CAD pattern simulation to cut physical sampling lead times down from 21 days to under 5 days, accelerating time-to-market.
From tech-pack consultation to international customs clearance, our streamlined OEM workflow guarantees total risk mitigation.
Our engineering team analyzes vector artwork, fabric weight targets, and seam requirements. We optimize grading charts across XS to 5XL to eliminate fitting anomalies.
Physical counter-samples are produced using exact mass-production machinery and target raw materials. Production starts only after formal buyer sign-off.
Computerized multi-head cutting tables and automatic flatlock stitching lines ensure dimensional variance stays strictly within ±2mm tolerances.
Inline inspections occur at cutting, printing, and sewing stages, culminating in a comprehensive final AQL 1.5/2.5 statistical audit prior to carton sealing.
Private label execution including heat-transfer neck tags, woven side labels, custom hangtags, scannable EAN/UPC barcodes, and retail polybags.
Seamless freight management offering EXW, FOB, CIF, or DDP air/sea/courier delivery with complete customs documentation and HS code accuracy.
Comprehensive answers regarding order execution, compliance, material sourcing, and private label support.
Submit your tech packs, sample requests, or custom product briefs directly to our senior manufacturing engineers. Receive direct factory quotes within 24 hours.
Contact Us