Industrial-grade construction, reinforced stress points, and customizable branding tailored for high-volume wholesale and private label clients.
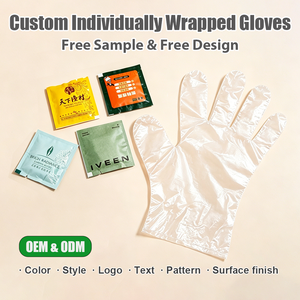
Multi-purpose high-density polyethylene protective gear designed for hygienic sports equipment handling and catering.
Contact Us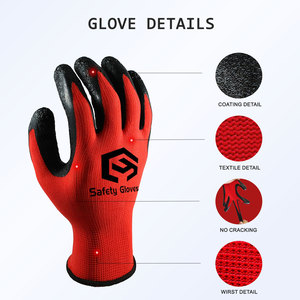
Heavy-duty crinkle-coated grip technology for material handling, equipment logistics, and sports gear management.
Contact Us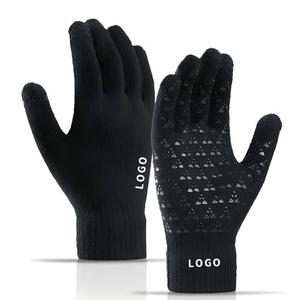
Thermal knit athletic utility gloves with anti-slip silicone grip printing and conductive touchscreen fingertips.
Contact Us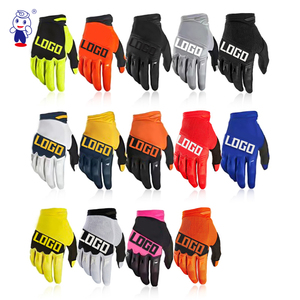
Ergonomic high-impact outdoor sports gloves featuring reinforced palm panels and dynamic ventilation channels.
Contact Us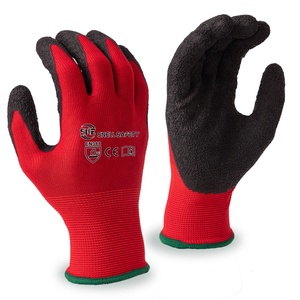
Industrial-grade grip protection with breathable backhands, optimized for tactical gear transport and heavy equipment.
Contact Us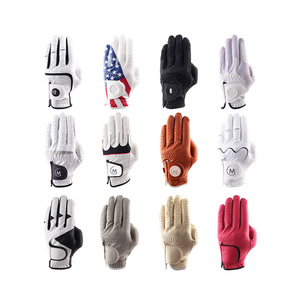
Ultra-soft Cabretta sheepskin leather golf gloves engineered for maximum tactile feedback and moisture dispersion.
Contact Us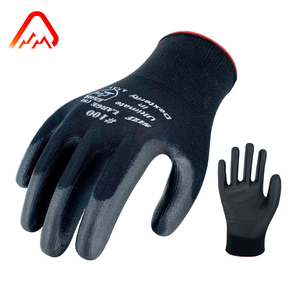
Certified EN388 protective work gloves with seamless nylon liner and anti-abrasion polyurethane coating.
Contact Us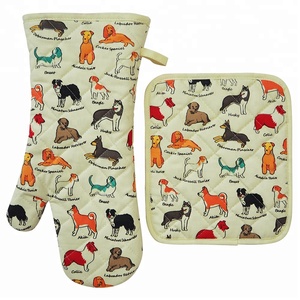
Thermal insulation cooking mitts and pot holders crafted from heavy-duty quilted cotton with anti-slip silicone texturing.
Contact UsA comprehensive white paper for procurement officers, global sports brands, gear distributors, and athletic academies.
Modern sports equipment logistics demand bag solutions capable of withstanding severe environmental stress, dynamic weight loads, and friction abrasion. Ball bags—ranging from high-capacity mesh sacks holding 10 to 15 inflated Size-5 soccer balls to heavy-duty water-resistant ball backpacks—serve as the foundation for team logistics worldwide. Selecting the right manufacturing partner involves analyzing textile denier specs, coating technologies, seam reinforcement methodologies, and compliance integrity.
The durability of a ball bag depends heavily on its core textile density and weave architecture. Our production lines primarily utilize three core synthetic material classes, engineered to meet distinct commercial specifications:
| Material Variant | Tensile Strength (N/5cm) | Water Resistance (Hydrostatic) | Optimal Application | Eco-Compliance |
|---|---|---|---|---|
| 600D PU Polyester | 1200 N | 3,000 mm H2O | Club Ball Backpacks & Duffels | REACH / RoHS compliant |
| 1680D Ballistic Nylon | 2400 N | 10,000 mm H2O | Heavy-Duty Team Equipment Carts | Standard Synthetic |
| Reinforced PVC Mesh | 850 N | Breathable Drainage | Bulk Soccer/Basketball Sacks | Phthalate-Free PVC |
| GRS Certified rPET 600D | 1150 N | 3,000 mm H2O | Sustainable Brand Lines | 100% GRS Recycled |
Anticipating structural shifts in global sports gear supply chains, material innovations, and commercial purchasing strategies.
Traditional needle stitching creates micro-perforations that reduce fabric integrity under heavy weight. Future manufacturing trends lean heavily toward sonic welding and thermo-taped waterproof seams, increasing load capacity by up to 35% while eliminating seam fraying.
Global sports leagues and retail conglomerates now require traceable post-consumer recycled fabrics. Our factory integrates blockchain-verified raw material sourcing, giving OEM clients verified certifications for marketing and environmental compliance.
Modern ball bags have evolved from simple drawstring sacks into multi-functional gear hubs featuring separate ventilated compartments for cleat storage, padded laptop sleeves, water-resistant ball cages, and internal mesh organizers for coaching gear.
Combining decades of OEM heritage, automated cutting machinery, and comprehensive compliance standards to deliver reliable quality on every order.
Our facility operates under audited social compliance standards (BSCI) and ISO 9001 quality management systems. Every batch undergoes strict AQL 1.5/4.0 inspections before container loading.
We provide comprehensive branding techniques including 3D screen printing, high-density embroidery, rubberized patch molding, custom zipper pulls, woven brand labels, and retail packaging inserts.
Utilizing laser-guided pattern cutters, digital stitching templates, and high-speed multi-head embroidery machines, our factory maintains exact dimensional tolerances across large-volume production runs.
Direct technical answers addressing minimum order quantities, lead times, custom branding, and shipping logistics.
Our standard production MOQ is 500 units per style for fully custom bag designs, including custom dye colors and specific material builds. For standard catalog bag patterns with custom logo printing, flexible MOQs start at 200 units per order.
Pre-production sample creation generally takes 7 to 12 working days following digital tech-pack approval. Once the physical pre-production sample is approved, bulk manufacturing requires 25 to 35 working days depending on order volume and customization complexity.
Our in-house quality assurance laboratory performs static weight load testing (up to 50kg held for 48 hours), dynamic drop testing from a height of 1.5 meters, zipper cycle endurance tests (minimum 5,000 pulls), and fabric tensile tear testing per ISO standards.
Yes. We stock GRS-certified 100% recycled 600D and 1200D rPET fabrics. We supply full transaction certificates (TC) tracking raw materials from post-consumer PET collection to the finished exported product.
We offer heavy-duty screen printing, heat transfer vinyl, 3D rubberized PVC patches, woven jacquard labels, high-density embroidery, molded metal/plastic zipper pulls, and custom printed interior lining fabrics.
We regularly handle shipments under EXW, FOB (Ningbo/Shanghai/Shenzhen), CFR, CIF, and DDP (Delivered Duty Paid) terms. Our logistics team handles all customs documentation, export declarations, and direct warehouse delivery.
Partner with China’s leading equipment bag factory. Contact our engineering team today to receive physical material swatches, digital mockups, and a competitive factory-direct quote.