Direct Factory Sourcing with Flexible MOQ, CE Compliance, and Private Label Customization
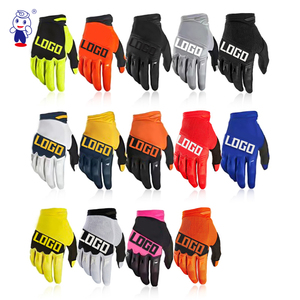
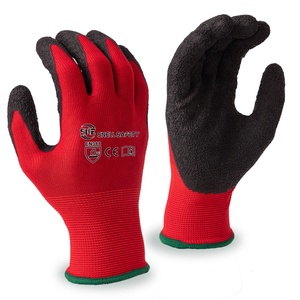
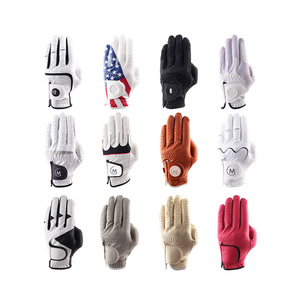
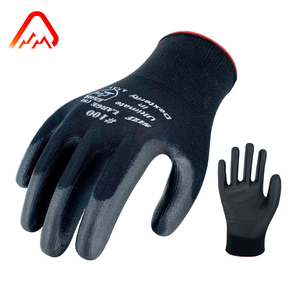
In the evolving landscape of international commercial trade, selecting a certified fitness gear manufacturer requires rigorous technical scrutiny. As an established OEM/ODM enterprise rooted in the historical manufacturing hub of Sialkot, Pakistan, our infrastructure integrates legacy craft mastery with state-of-the-art polymer science and automated stitching assembly. Operating under strict compliance frameworks, including BSCI (Business Social Compliance Initiative) and OHSAS 18001 / ISO 45001 occupational safety benchmarks, our facilities ensure zero supply disruption while maintaining pristine ethical manufacturing standards.
CE Marking for athletic protective equipment and tactical safety gear is not merely a label; it represents an exhaustive verification process under European Regulation (EU) 2016/425. Our manufacturing facility adheres to specific EN standards—such as EN388 for mechanical risk protection, EN420 for general glove ergonomics, and specialized shock-absorption criteria for impact-mitigating fitness apparel. By maintaining in-house testing laboratories equipped with pneumatic tensile testers, friction abrasers, and dynamic impact towers, every production batch achieves verified repeatability before leaving our loading docks.
Our factory floor eliminates intermediary brokerage overhead through complete vertical integration. Our engineering pipeline encompasses six key modules:
Global buyers, brand procurement directors, and tier-one distributors are navigating structural shifts in material compliance, geopolitical sourcing diversification, and environmental regulations. Sourcing managers must align their supply chains with key macroeconomic and technical procurement trends driving the activewear and protective equipment sectors:
Regulatory oversight across the European Union and North America continues to tighten regarding hazardous chemical residues in wearable fitness accessories. European REACH Annex XVII guidelines mandate strict thresholds for Polycyclic Aromatic Hydrocarbons (PAHs), phthalates, azo dyes, and heavy metals. Future-proof procurement requires direct integration with raw material mills that supply certified eco-friendly TPU, solvent-free PU, and bio-based synthetic polymers. Our R&D department continuously replaces traditional petroleum-based rubbers with sustainable natural latex compounds and recycled polyester yarns (GRS Certified), offering environmental compliance without sacrificing mechanical tear resistance.
Corporate Sustainability Reporting Directives (CSRD) are compelling multinational sports equipment brands to map Scope 3 emissions down to the raw fiber level. Sourcing managers are migrating away from unverified trading entities toward direct manufacturers capable of issuing Material Safety Data Sheets (MSDS) and transparent chain-of-custody documentation. By centralizing raw material storage, cutting, assembly, and packaging within our Sialkot manufacturing complex, we provide complete auditing transparency for international compliance teams.
The era of 10,000-piece single-SKU commitments is diminishing. Dynamic e-commerce inventory models require agile production scheduling, quick prototyping runs (7–14 days), and flexible minimum order quantities (MOQs) that permit colorway splits and multi-size curves within a unified master purchase order. Our modular production lines are configured to handle both high-volume OEM contracts and targeted boutique brand launches without compromising line efficiency.
Performance equipment development has evolved from basic cut-and-sew operations into sophisticated biomechanical engineering. Modern athletes and industrial workers demand gear that provides micro-climate temperature regulation, kinetic shock dampening, and ergonomic freedom of movement.
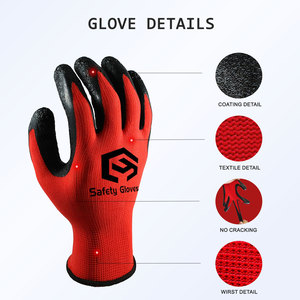
In products such as goalkeeper gloves, weightlifting grips, and specialized industrial work gloves, latex formulation governs performance. Our laboratory incorporates German-engineered latex foams infused with micro-encapsulated sticky agents, delivering superior tackiness under both wet and dry conditions. For high-wear utility gloves, crinkle latex coatings and micro-porous nitrile dip processes are optimized to yield a Shore A durometer rating that balances flexibility with extreme puncture resistance.
Traditional stitched seams often create localized pressure points, skin friction, and structural failure zones. We utilize high-gauge computerized knitting technology to produce seamless base layers, winter touch-screen sports gloves, and joint support sleeves. By varying yarn tension dynamically during the knitting cycle, targeted compression zones support musculoskeletal alignment, accelerate venous blood return, and minimize muscle fatigue during high-intensity training.
| Product Category | Primary Materials | Testing Protocol | CE / Compliance Grade | Key Performance Feature |
|---|---|---|---|---|
| CE Safety & Work Gloves | Crinkle Latex / PU / 13-Gauge Nylon | EN388:2016 (Abrasion/Cut/Tear) | Category II / CE Approved | Anti-slip grip, tactile sensitivity, high abrasion durability. |
| Tactical & Moto Gear | Reinforced Synthetic Leather / Carbon Knuckle | EN13594 Impact Protection | CE Level 1 / Level 2 | Kinetic shock absorption, high tensile tear strength. |
| Elite Athletic Gloves | German Quartz Latex / Neoprene / Mesh | ISO 13934-1 Seam Strength | REACH Compliant / OEKO-TEX 100 | Hyper-cohesion grip foam, ergonomic backhand flexing. |
| Thermal & Utility Gear | Aramid Fiber / Heavy Cotton / Silicone | EN407 Thermal Resistance | Contact Heat Level 2+ | Heat mitigation up to 500°C, food-grade silicone grip. |
For over a century, Sialkot, Pakistan, has maintained an unassailable reputation as the premier global cluster for sporting goods manufacturing, supplying major international tournaments, elite professional leagues, and top-tier safety gear brands worldwide. The region’s competitive advantage resides in a dense ecosystem of specialized material tanneries, polymer compounders, precision die-makers, and a highly skilled workforce whose specialized hand-stitching and patterning skills have been perfected over generations.
Our manufacturing unit merges this deep industrial heritage with modern industrial engineering. By synthesizing localized material sourcing advantages with modern ISO-aligned quality systems, we provide our international partners with an optimal ratio of cost efficiency, mechanical product excellence, and reliable lead-time execution. Whether your procurement strategy focuses on scaling an established activewear label or contracting robust industrial gear for global distribution, our enterprise delivers certified performance engineered to excel in demanding commercial environments.
Submit your technical specifications, sample requests, or bulk RFQs directly to our engineering and export merchandising teams.
Send an Inquiry