Explore our high-performance B2B duffel bag formulations, safety equipment carriers, and professional athletic luggage engineered for private-label distributors worldwide.
In the global supply chain for athletic, industrial, and tactical luggage, obtaining true CE Certification is not merely a marketing sticker—it represents a stringent validation of physical durability, chemical safety, ergonomics, and structural integrity under international regulatory frameworks. As a premier direct OEM/ODM exporter based out of the world-renowned industrial manufacturing cluster in Sialkot, Pakistan, Spogen Pvt Ltd manufactures professional duffel bags, athletic gear holdalls, and equipment carriers engineered to meet demanding European Union (EU) Directives, REACH standards, and ISO quality benchmarks.
Navigating global procurement requires direct accountability. Unlike trading intermediaries or unverified third-party agents, our unified manufacturing facility manages every phase of production under one roof: from initial technical pattern creation (Tech-Pack design), hydraulic die-cutting, automated embroidery, high-frequency 3D embossing, to ultrasonic seam sealing and final AQL 2.5 quality control checks.
International sourcing managers, sports brand buyers, and corporate procurement directors face substantial supply chain risks, including material delamination, fabric tearing under heavy load, zipper failure, and non-compliance with EU chemical hazardous material bans (AZO dyes, Phthalates, Heavy Metals). Our engineering team mitigates these challenges through rigorous pre-production material science:
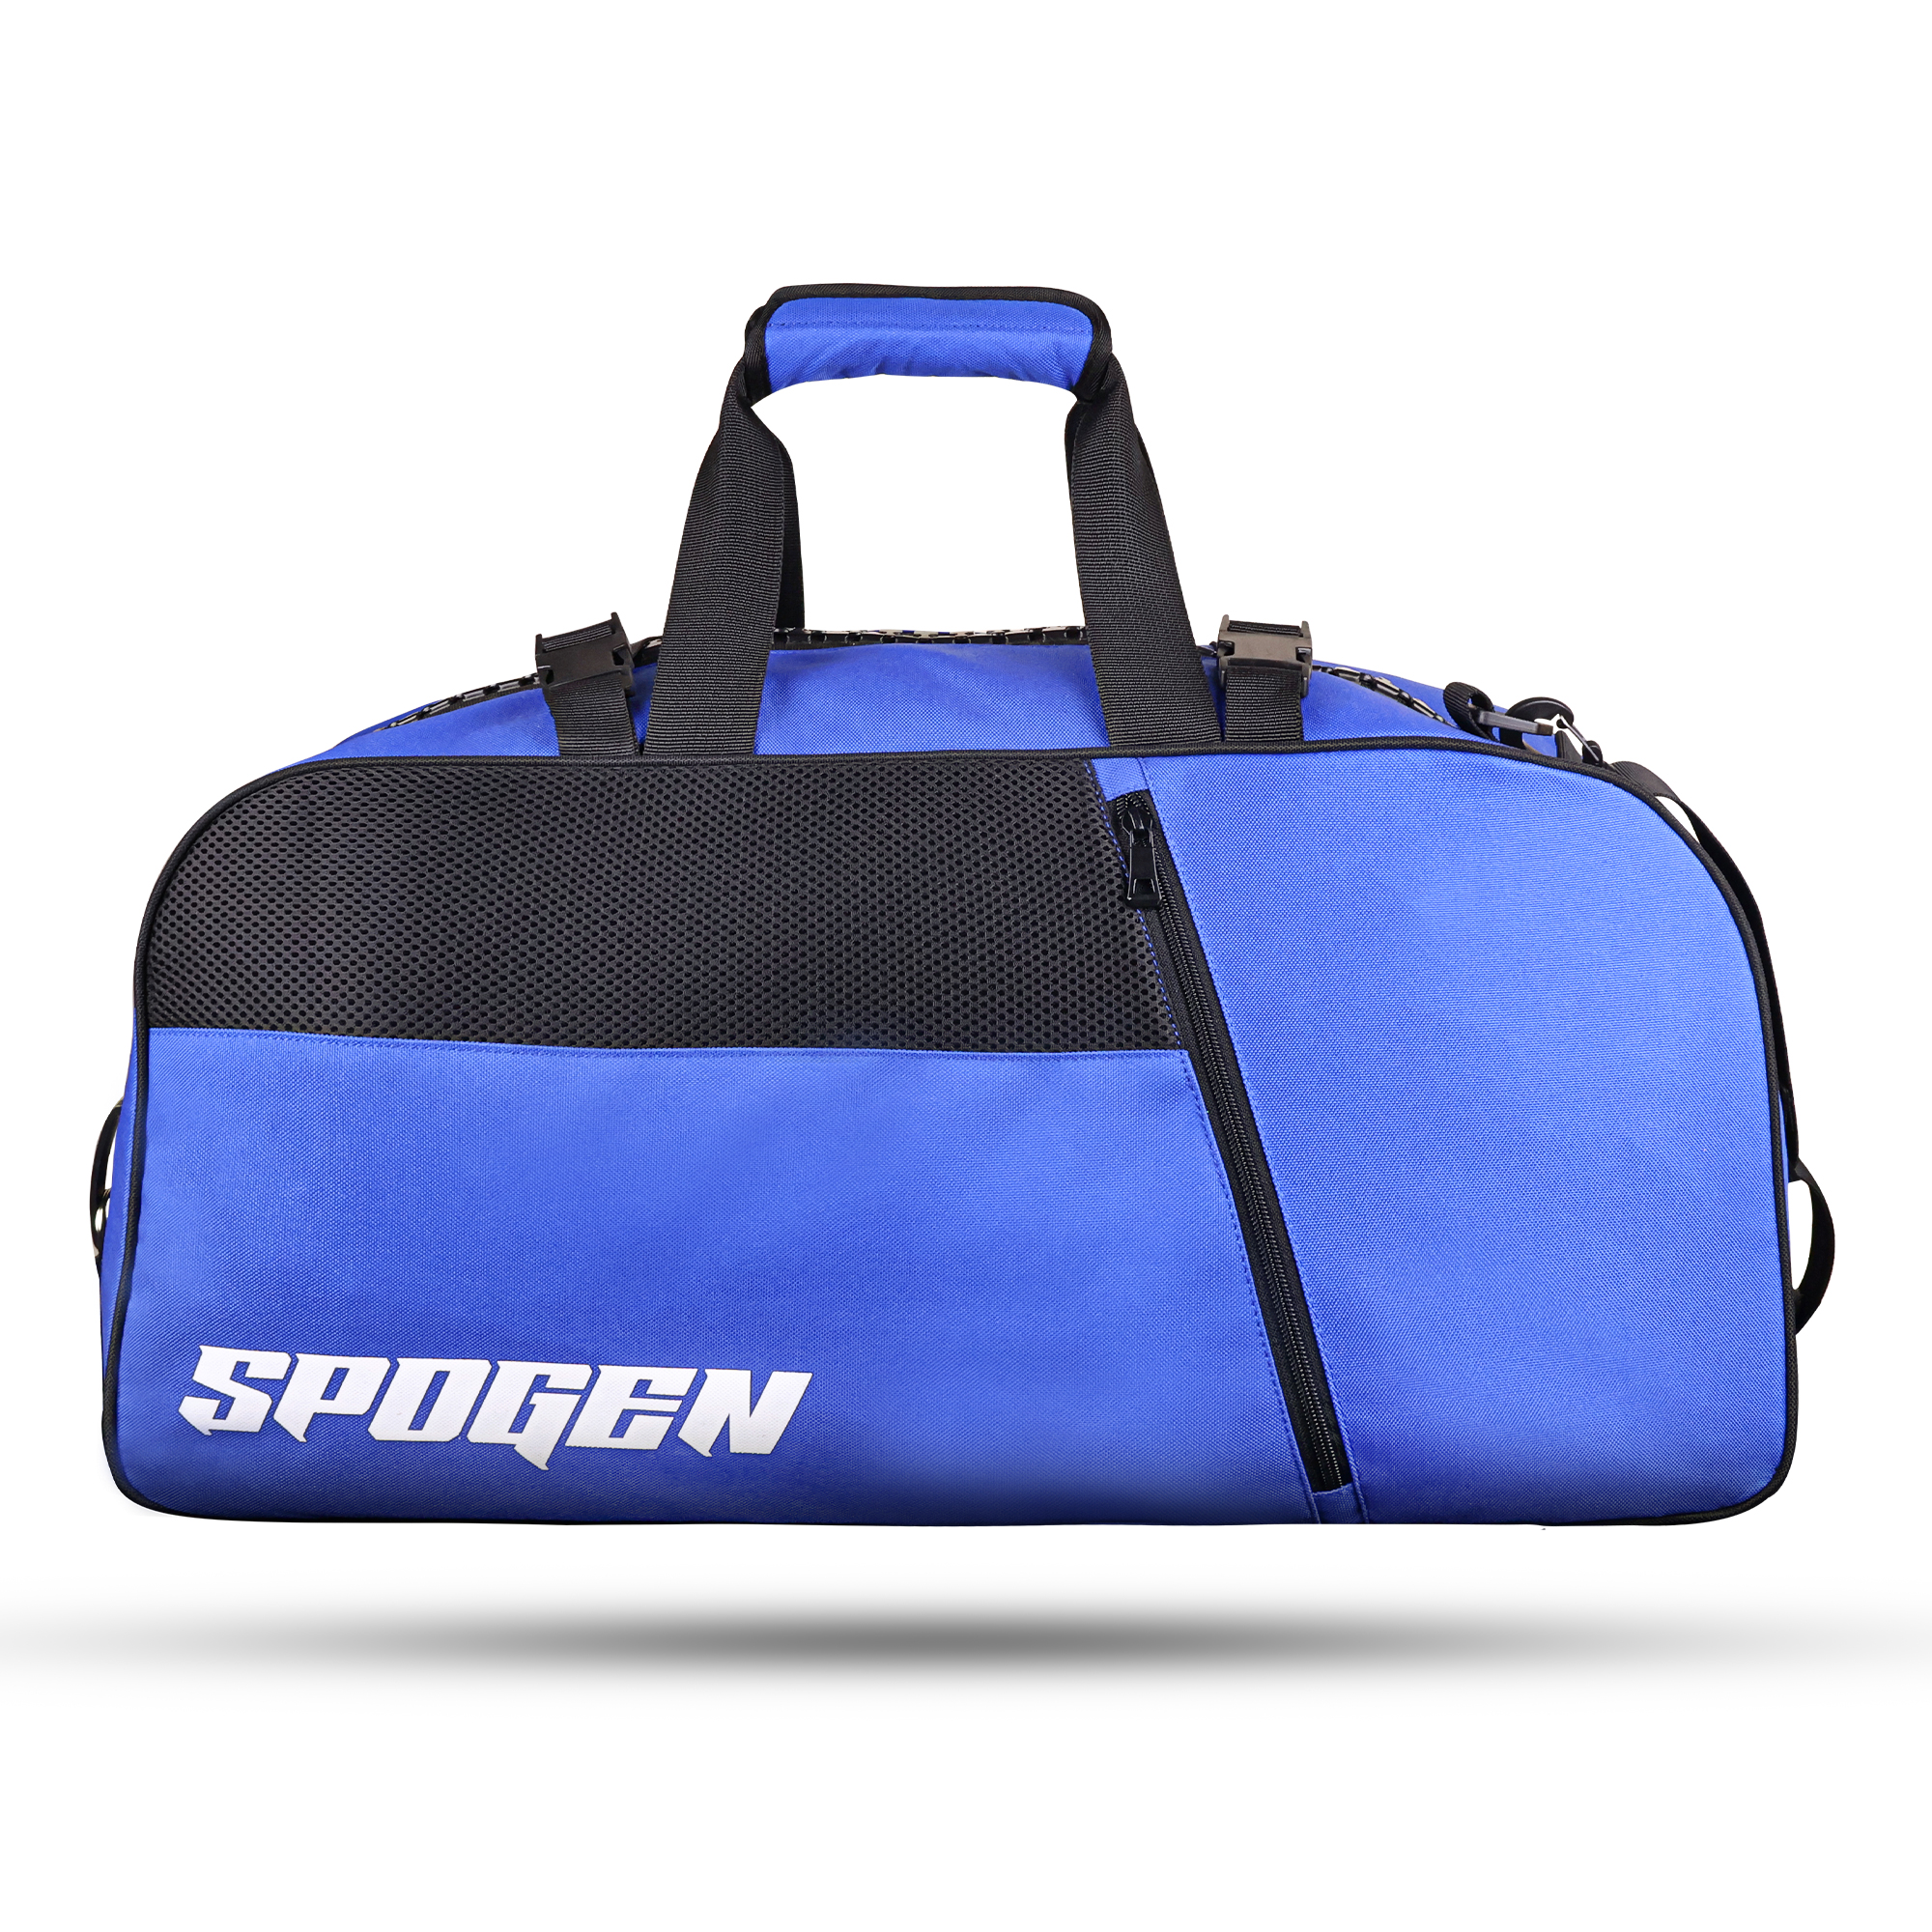
To assist procurement managers in establishing baseline specs for RFQs (Request For Quotes), the comparison matrix below outlines the engineering differences engineered into our CE-grade exports:
| Specification Parameter | Standard Commercial Duffel | Spogen CE Certified Industrial Duffel |
|---|---|---|
| Outer Shell Fabric | 300D - 600D Polyester (Low PVC back) | 900D - 1600D Cordura / TPU Coated Recycled Nylon |
| Tensile Strength (ISO 13934) | < 600 N Strain Limit | > 1400 N High-Tenacity Break Point |
| Waterproofing Level | Water-Repellent Spray Coating | Hydrostatic Head > 10,000 mm + Sealed Seams |
| Zippers & Hardware | Standard Nylon Coil / Zinc Alloy Sliders | YKK AquaGuard® / Anti-Corrosion Heavy-Duty Steel |
| Chemical Safety Certification | Unverified / Untested Raw Textiles | REACH SVHC Compliant / AZO-Free / OEKO-TEX Standard 100 |
| Load-Bearing Strap Construction | Single Stitch PP Webbing | Cross-Box Bar-Tacked High-Density Polypropylene |
Ethical workplace standards, fair wages, zero child labor, and safe factory conditions verified under European BSCI framework audits.
Occupational health and environmental safety systems operating across all cutting, printing, stitching, and packing floors.
Seamless export documentation, customs clearance, HS Code classification, and door-to-door delivery across Europe, USA, UK, and UAE.
As sustainability mandates tighten and consumer expectations evolve, B2B buyers must align with manufacturers pioneering next-generation materials and modular structural design.
The transition from virgin petroleum-based polyester to Global Recycled Standard (GRS) RPET derived from post-consumer plastic bottles is now a requirement for EU brands. Spogen offers full chain-of-custody documentation for GRS 4.0 woven textiles, reducing carbon footprints by up to 45% per unit without compromising tensile durability.
Modern sports team duffels and tactical luggage are shifting away from static open-cavity designs toward dynamic modularity. Procurement calls now prioritize detachable hydro-isolated wet/dry shoe pods, insulated nutrition pockets, and laser-cut MOLLE webbing systems for external gear attachment.
Traditional needle-and-thread stitching creates micro-perforations that compromise water resistance over time. Next-gen CE certified duffels utilize high-frequency ultrasonic seam sealing and hot-melt TPU taping to craft 100% airtight, waterproof dry-bag holdalls suitable for marine, outdoor, and extreme weather use.
Combining ergonomic load distribution, smart security hardware, and high-durability polymers to deliver unmatched performance in commercial transport.
Eliminating carrier fatigue through stowable, contoured EVA-padded shoulder straps that seamlessly transition a traditional duffel into an ergonomic backpack within seconds.
Integrating silver-ion matrix coatings inside damp laundry and footwear compartments, prohibiting bacterial growth and odor buildup during multi-day team travel.
Employing compression-molded EVA top lids and bases to absorb heavy kinetic impacts during transit, safeguarding sensitive electronic equipment, optics, and sports gear.
From technical CAD tech-packs to containerized global dispatch, our standardized workflow guarantees sample-to-production fidelity for every bulk order.
Digital proofing, pattern grading, color matching (Pantone TPX), and selecting Denier ratings, PVC/TPU coatings, and custom hardware finishes.
Precision hydraulic press cutting of fabric panels, inner linings, foam padding, and reinforcement gussets ensuring razor-sharp dimensional accuracy.
Applying high-density screen printing, 3D rubber logo badging, heat transfer sublimation, or thermal embossing across custom outer panels.
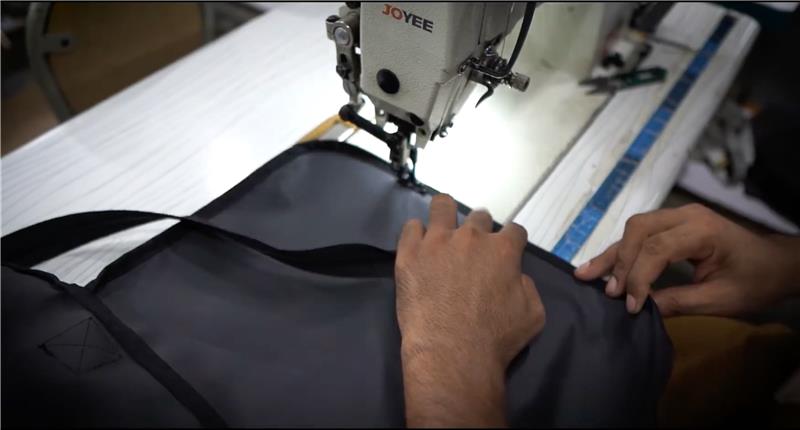
Assembly using automated programmable sewing machinery, nylon bonded threads, bar-tack stress reinforcement, and hot-air seam taping.
Rigorous quality assurance verifying zipper pull resistance, seam strength, water repellency, logo alignment, and dimensional tolerances.
Polybag sealing, barcode hangtag attachment, master carton drop-test validation, and dispatch via Sea (FOB/CIF) or Air Express (DDP).
Expert guidance addressing common inquiry parameters from procurement officers, sourcing managers, and brand directors.
CE Certification for bags (depending on intended application such as industrial safety equipment transit or personal protection gear storage) mandates compliance with EU General Product Safety Regulations (GPSR), REACH Chemical Directives (EC 1907/2006) prohibiting harmful phthalates, heavy metals, and AZO colorants, as well as mechanical strength testing (ISO 13934) ensuring seams and load-bearing handles do not rupture under specified weight capacities.
Our standard Minimum Order Quantity (MOQ) for custom private-label duffel bags is typically 100 to 200 pieces per design/colorway, depending on fabric specification and customization complexity. We support split-size and multi-colorway allocations within a master production run to accommodate expanding product lines.
Pre-production physical samples with full private label branding are typically finalized within 7 to 14 working days after Tech-Pack approval. Bulk factory production generally ranges between 20 to 35 working days depending on order volume, fabric custom-dyeing requirements, and peak seasonal schedules.
Yes. We provide complete technical dossier documentation including material safety data sheets (MSDS), REACH chemical compliance verification, lab test certificates for hydrostatic waterproof ratings, and factory audit reports (BSCI, OHSAS 18001) required for smooth European Union and US Customs import clearance.
We provide full-spectrum private labeling capabilities, including 3D molded silicone badging, high-density silk screen printing, thermal heat-transfer sublimation, laser-engraved metal zipper pullers, woven inner branding labels, custom printed linings, and customized barcode hangtags with retail-ready polybag or box packaging.
We work flexibly across all standard Incoterms including FOB (Free on Board) Karachi / Lahore, EXW (Ex-Works), CIF (Cost, Insurance & Freight), and DDP (Delivered Duty Paid) directly to buyer warehouses or distribution fulfillment centers across Europe, North America, Oceania, and the Middle East.
Partner directly with Sialkot's premier BSCI & ISO certified manufacturing facility. Request technical specs, physical material samples, or an immediate RFQ quotation from our engineering team.